language
Perforated Anti-slip Walkway Plank Punching and Roll Forming Line
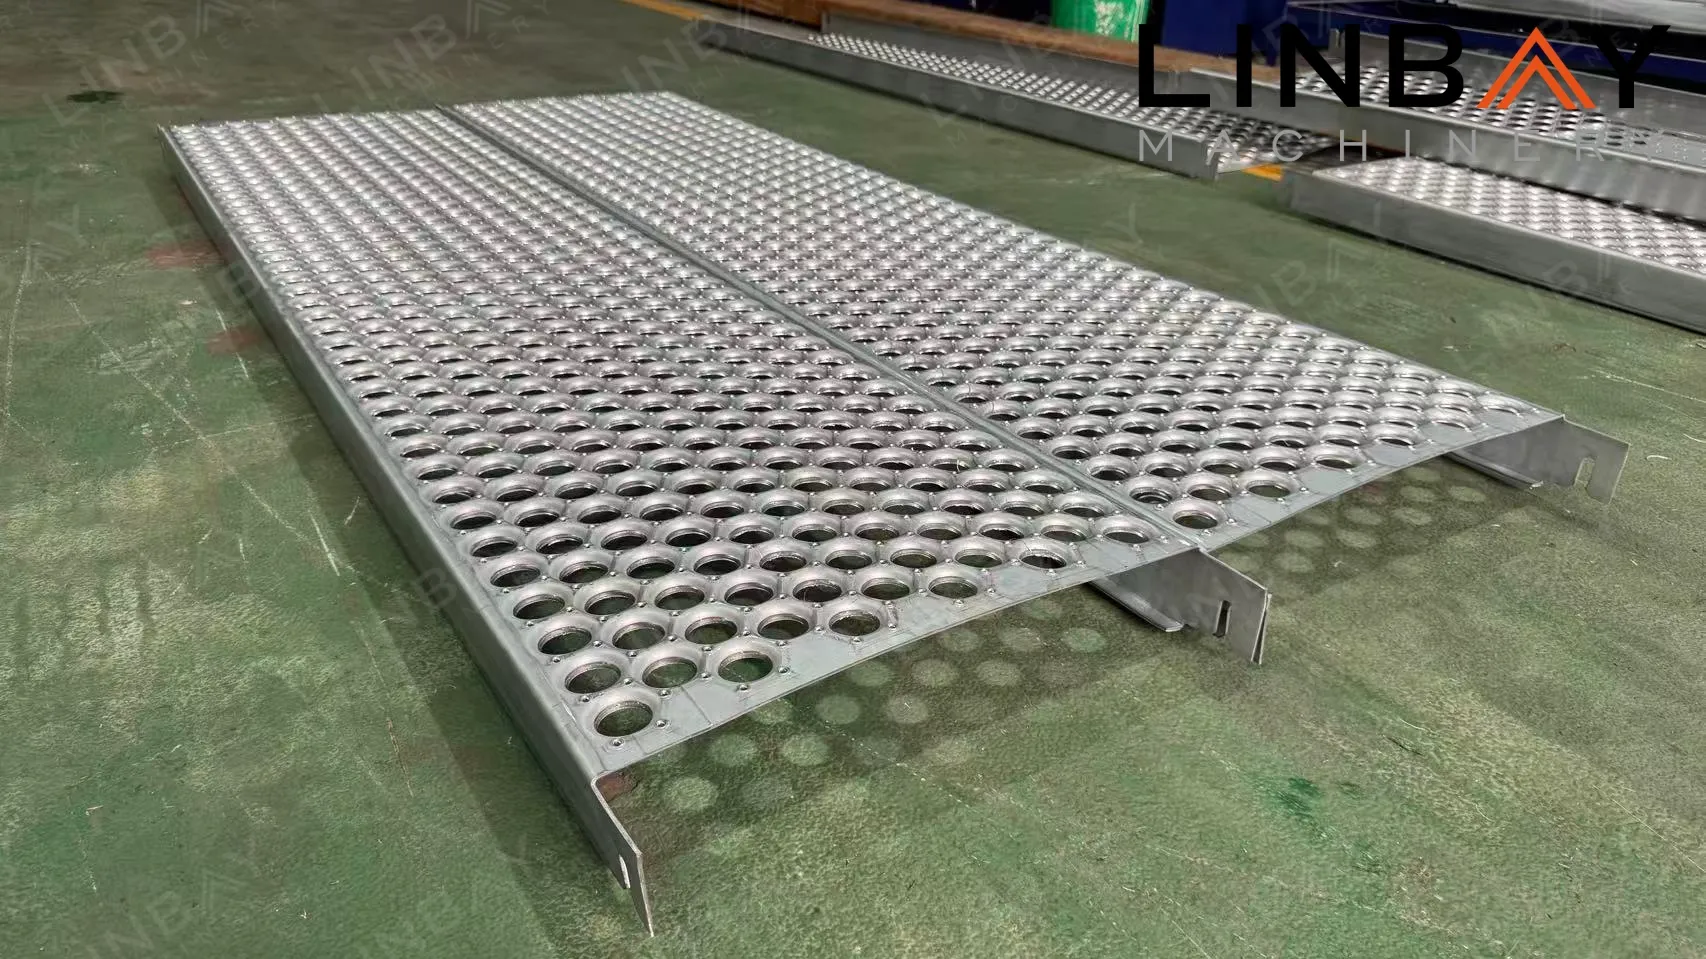

The Perforated Anti-slip Walkway Plank Roll Forming Line is designed for the production of heavy-duty galvanized steel walkway planks / safety grating panels / anti-slip step planks. The finished profiles feature densely arranged perforated and raised holes, providing an anti-slip surface while allowing drainage and ventilation.
The finished planks can be used not only for industrial walkways and working platforms, but also as stair treads for warehouse racking and mezzanine systems, as well as access steps and step plates for trucks. Their perforated anti-slip surface makes them suitable for applications where secure footing and structural strength are required.
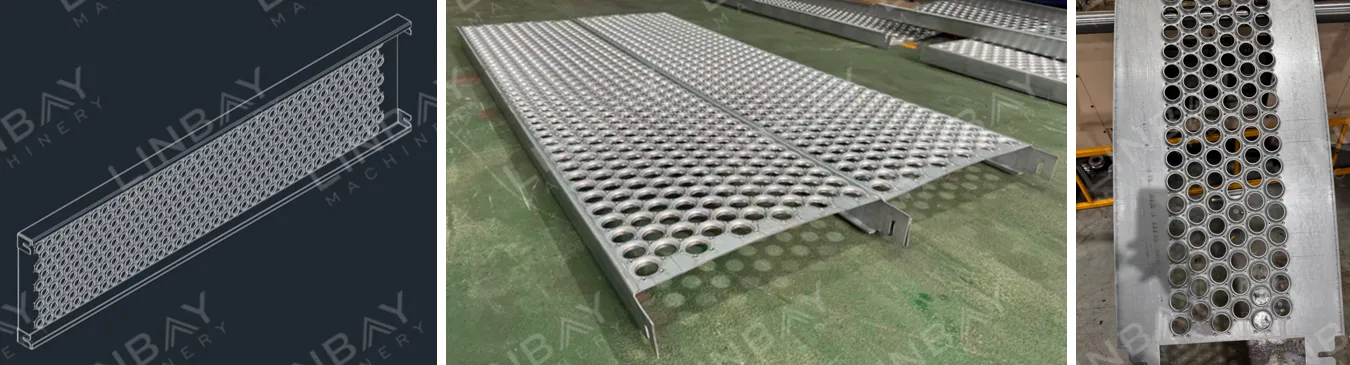
Designed for processing 3 mm galvanized steel, this production line integrates coil decoiling, leveling, strip joining, precision servo feeding, punching, roll forming and cutting into a complete production process. A 400-ton punch press with progressive die performs continuous perforation before the material enters the roll forming section, allowing the perforated pattern and final profile to be produced efficiently on one integrated line.
Decoiling → Leveling → Butt Welding → Servo Feeding → Progressive Die Punching → Roll Forming → Hydraulic Cutting → Output
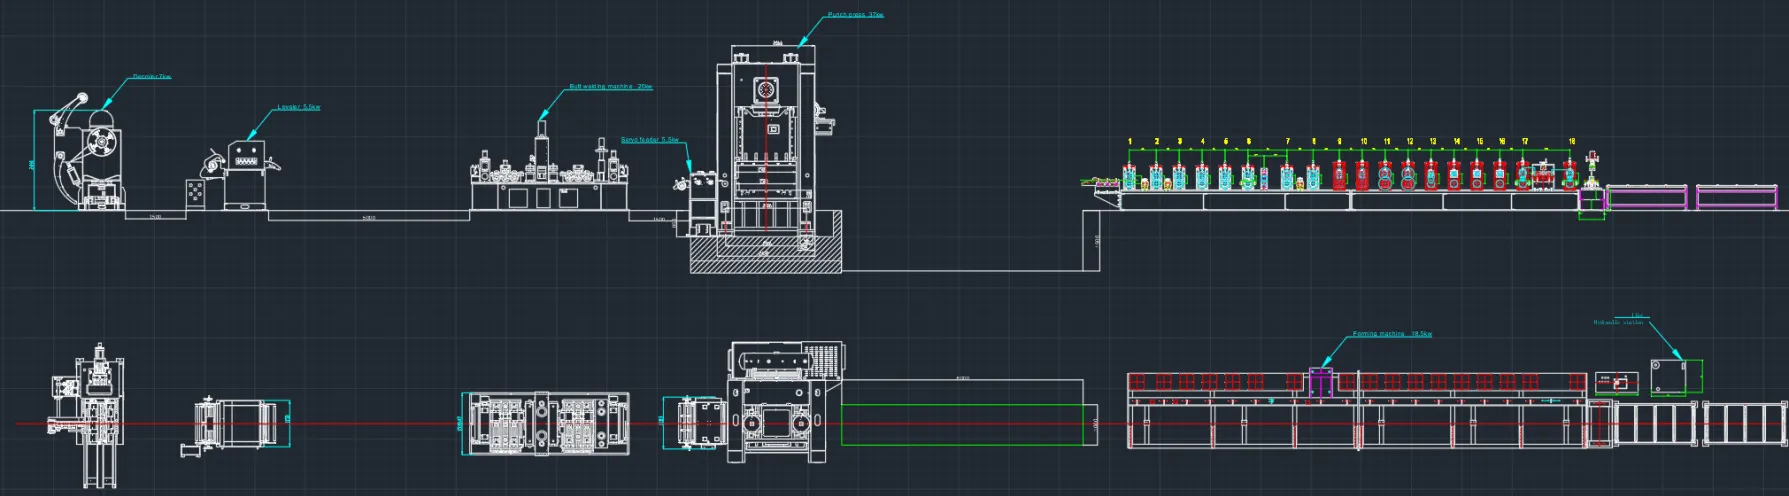
Integrated Punching and Roll Forming: Combines material preparation, precision feeding, perforation and profile forming in one complete production system.
Heavy-duty Material Processing: Designed for 3 mm galvanized steel with a robust forming structure and gearbox transmission.
Continuous Perforation with 400-ton Punch Press: The ETD-400 punch press works with a progressive die to continuously produce the characteristic perforated and raised anti-slip pattern. Punching speed reaches 50–70 strokes/min.
Precision Servo Feeding: A 5.5 kW Yaskawa servo feeding system provides accurate material positioning and consistent perforation spacing.
Heavy-duty Roll Forming System: The roll former adopts 18 forming stations, Cr12 rollers hardened to HRC58–62, Ø70 mm 40Cr shafts, gearbox transmission and an 18.5 kW forming motor.
Automatic Control System: Siemens PLC, MCGS HMI and Yaskawa frequency inverter provide convenient and stable production control.
| Parameter | Specification |
| Raw Material | Galvanized Steel |
| Material Thickness | 3 mm |
| Line Working Speed | 0–8 m/min with continuous perforation |
| Roll Forming Speed | 0–20 m/min |
| Decoiler Loading Capacity | 5 tons |
| Decoiler Hydraulic Motor Power | 3 kW |
| Leveling Motor Power | 3 kW |
| Servo Feeder Motor Power | 5.5 kW with reducer, Yaskawa |
| Servo Feeding Speed | 0–50 m/min, adjustable |
| Feeding Accuracy | ≤ ±0.1 mm within 200 mm; ≤ ±0.2 mm within 500 mm |
| Punch Press Model | ETD-400 |
| Punching Force | 400 tons |
| Punching Speed | 50–70 strokes/min |
| Punch Press Motor Power | 18.5 kW, Siemens |
| Punch Die | Progressive die |
| Roll Former Structure | Cast iron stands |
| Forming Stations | 18 stations |
| Roller Material | Cr12, quenched, HRC 58–62 |
| Shaft Material | 40Cr, heat treated |
| Shaft Diameter | Ø70 mm |
| Driving System | Gearbox drive |
| PLC | Siemens |
| HMI | MCGS |
| Frequency Inverter | Yaskawa |
| Power Supply | 380 V, 50 Hz, 3 Phase (customizable) |
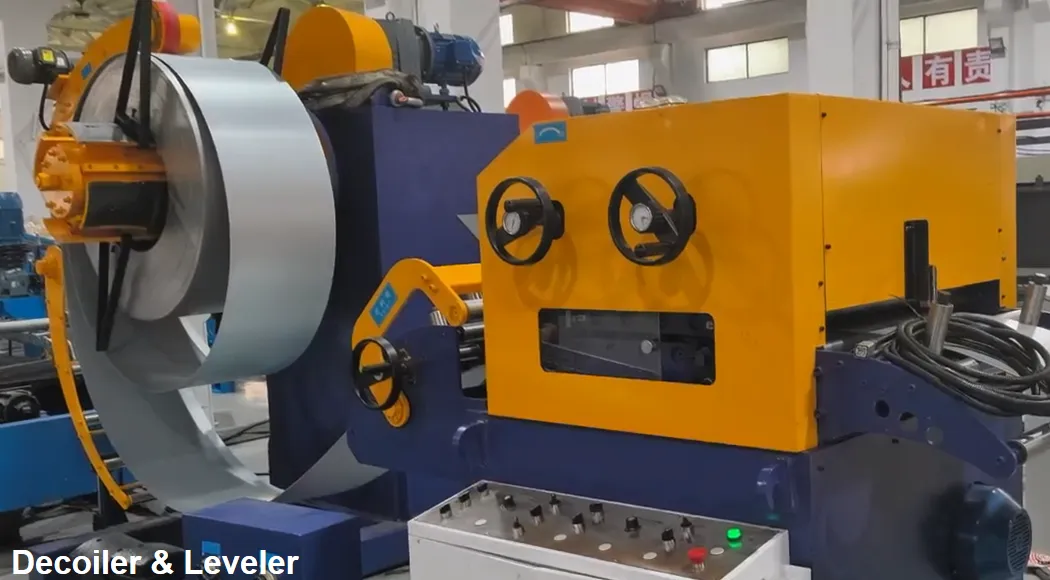
Hydraulic Decoiler and Leveler
The line starts with coil decoiling and leveling. The 5-ton hydraulic decoiler supplies material, while the leveling unit prepares the strip for accurate downstream feeding and punching.
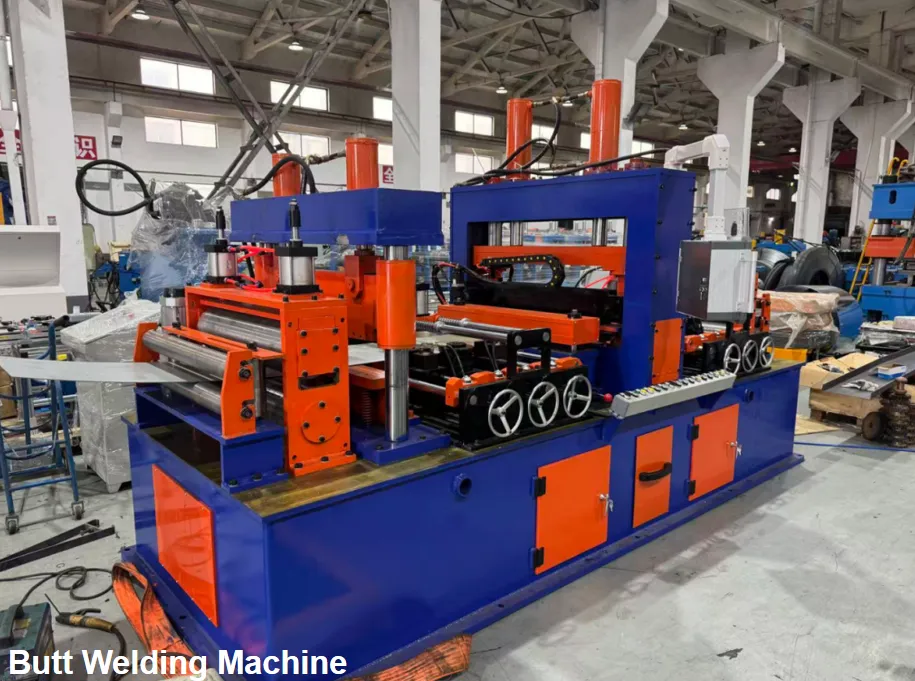
Butt Welding Machine
A butt welding machine is arranged between the leveling and servo feeding sections. It can join the tail end of one coil to the leading end of the next coil when required, facilitating continuous material feeding.
Servo Feeder
Driven by a 5.5 kW Yaskawa servo motor, the feeder provides accurate material positioning for consistent punching pitch and pattern.
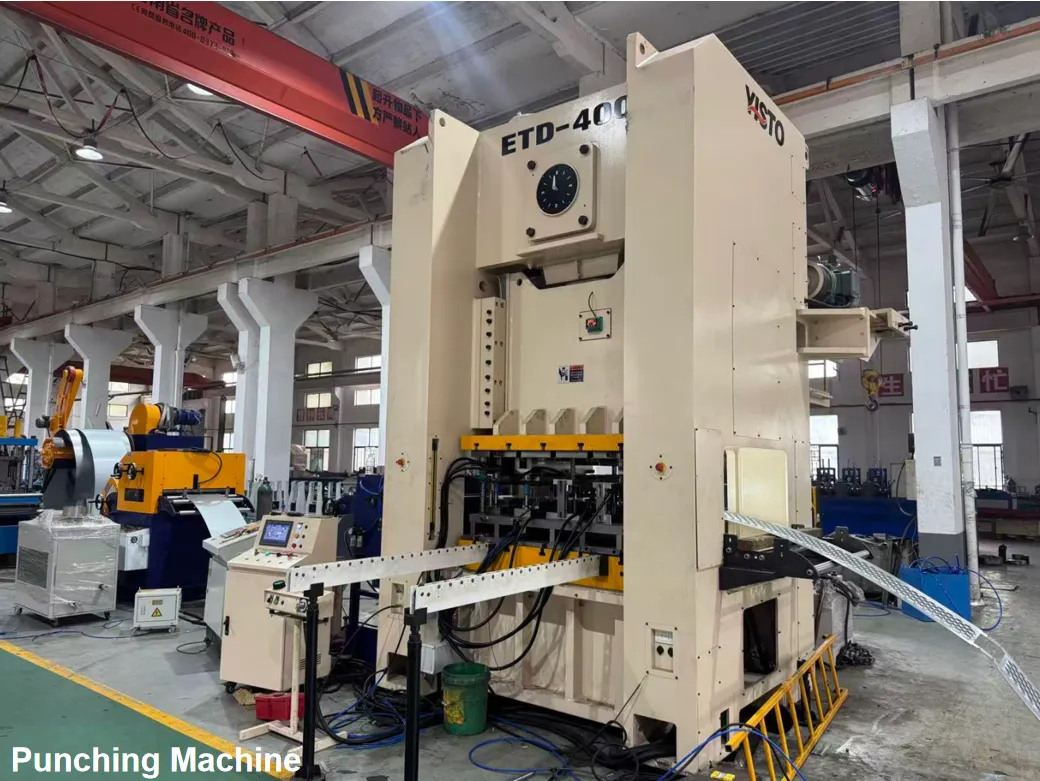
Punch Press and Progressive Die
The ETD-400 punch press provides 400 tons of punching force and works with a progressive die to produce the dense perforated and raised anti-slip pattern.
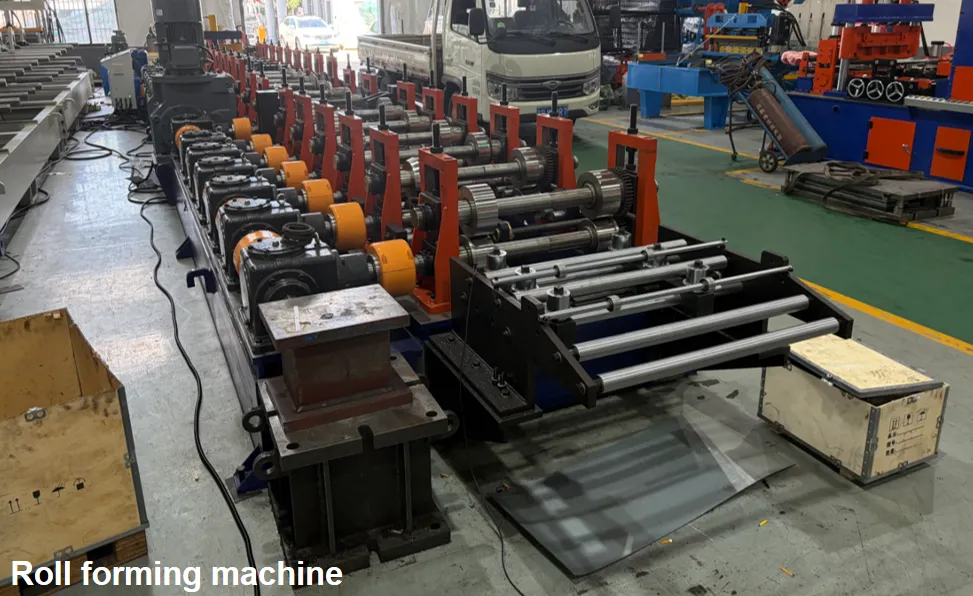
Roll Forming Machine
After punching, the perforated strip enters the roll former. The combination of 18 forming stations, Cr12 rollers, Ø70 mm 40Cr shafts, gearbox transmission and an 18.5 kW forming motor provides a robust forming system for 3 mm galvanized steel.
Hydraulic Cutting and Output
After roll forming, the finished profile is cut to the required length by the hydraulic cutting unit and transferred to the output tables.
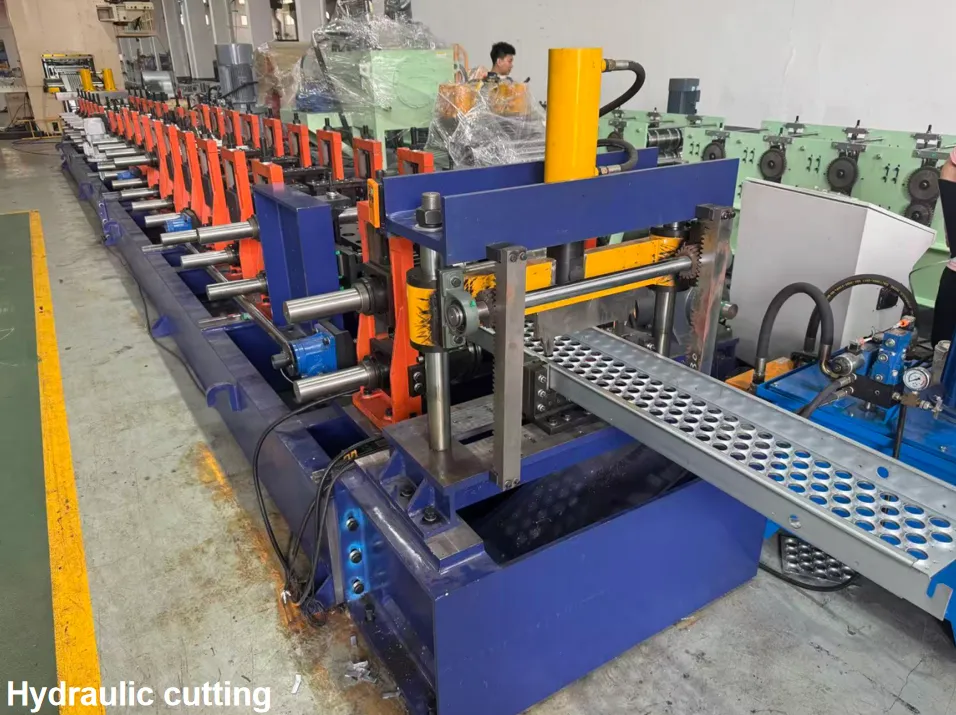
The finished perforated anti-slip plank combines a formed structural profile with a densely perforated surface. The raised perforated pattern improves grip while providing drainage and ventilation. Depending on the profile design and project requirements, the plank can be used as an industrial walkway panel, a stair tread for warehouse racking or mezzanine systems, or an access step for trucks.
· Industrial walkways and maintenance passages
· Warehouse racking and mezzanine stair treads
· Truck access steps and step plates
· Factory working platforms
· Equipment access platforms
· Elevated walkways and stairways
· Warehouse and production platforms
· Industrial safety flooring systems
LINBAY can customize the Perforated Anti-slip Walkway Plank Roll Forming Line according to the customer's profile drawing and production requirements. Profile dimensions, material specifications, punching patterns, production speed, electrical standards and other machine configurations can be adjusted according to the specific project.
Related Products


CONTACT US
Contact US
Product Information
Quantity
Unit
Piece
Support order samples, customization, wholesale direct, and complete payment. If the product you look for does not have corresponding customized content, pls fill out the form below to contact us, and we will reply ASAP.